



- Publisher:mzadmin
- Published on:2026-08-31
- Pageviews:8926
The correct welding method for cement electric poles
In the construction of transmission lines, cement poles with a length exceeding 15 meters often need to be transported in sections and welded on site. The welding joint is the weakest link in the mechanical performance of the entire pole, and it is also the key to determining the long-term safe operation of the line. As a professional cement pole manufacturer, we deeply understand the importance of welding quality - an unqualified weld can greatly reduce the load-bearing capacity of the entire line. From a professional perspective, we will summarize the correct process and technical points for welding the steel ring of cement electric poles.
Preparation before welding is the foundation of quality. Welding must be performed by professional welders holding corresponding qualification certificates, which is a mandatory requirement of national regulations. Welding rods should be selected from models that comply with national standards, such as E4303, and stored in moisture-proof boxes. Welding rods that are damp or have fallen off are strictly prohibited from use. Before welding, it is necessary to thoroughly remove rust, oil stains, and oxide layers from the welded joints of the steel ring and nearby areas. At the same time, check the overall levelness and concentricity of the rod section, align and align the docking steel rings, and control the welding gap between 2 and 5 millimeters. The deviation of the misalignment should not exceed 2 millimeters. After confirming the correctness, weld 3 to 4 evenly along the steel ring joint surface for fixation, and the welding rod used for spot welding must be consistent with the formal welding.
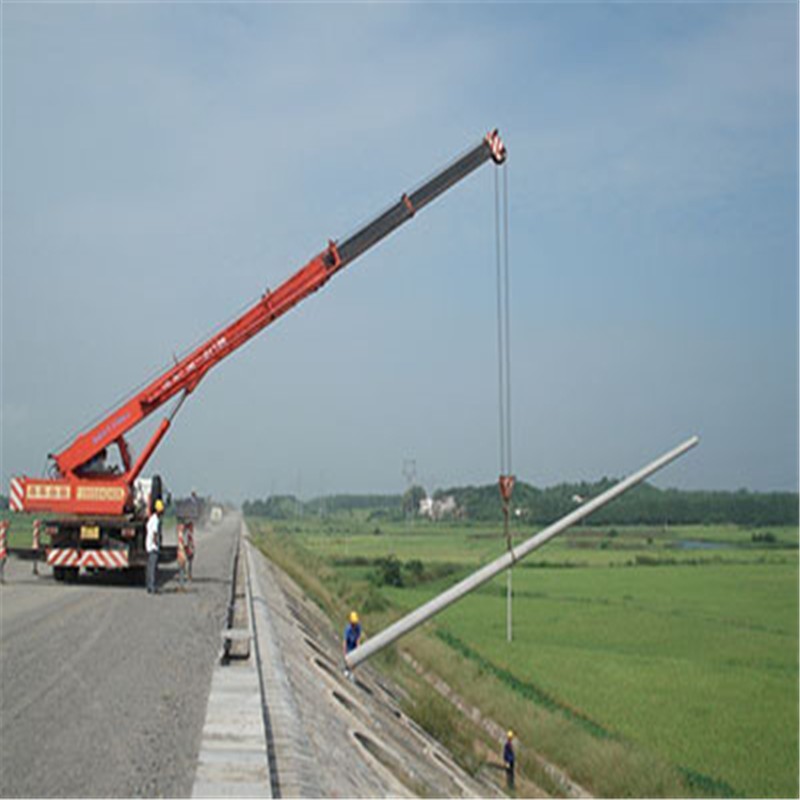
The welding process emphasizes symmetry and continuity. The formal welding should be carried out using arc welding, and symmetrical cross welding should be used from bottom to top. The starting point of each welding should be rotated about 100 millimeters in sequence, and the weld seam should be welded firmly after 3 to 4 cycles. This can effectively prevent one-sided overheating and bending deformation of the pole. When the thickness of the steel ring is greater than 6 millimeters, a V-shaped groove must be used for multi-layer welding. After each layer of welding is completed, the welding slag should be cleaned, and the joints of each layer of weld should be staggered by at least 50 millimeters to ensure penetration and no slag inclusion. When extinguishing the arc, be sure to fill the molten pool to avoid arc pit cracks. The welding current should be controlled between 200 and 250 amperes to prevent undercutting defects caused by excessive current. The entire weld should be completed continuously as much as possible, and the final formed weld should present a smooth, fine scale appearance.
Post weld inspection and corrosion prevention cannot be ignored. After welding is completed, place the pole on the ground level for inspection. The curvature of the entire pole must not exceed 0.2% of its total length. If it exceeds the standard, it must be cut and straightened before re welding. After the welding joint is completely cooled, the surface rust, welding slag, and oxide layer should be cleaned in a timely manner, and anti rust paint should be applied or other anti rust measures should be taken to prevent the joint from rusting and failing. Welders who pass self inspection should stamp a steel seal code on the designated area to ensure quality traceability.
The welding of cement poles is a highly technical and responsible concealed project. Standardized operation is not only related to the installation quality of electric poles, but also directly affects the service life of the line for decades. As a professional pole manufacturer, we always adhere to high standard welding processes, controlling the entire process from materials to construction, and providing you with safe and reliable connection guarantees. If you encounter any welding technical questions during construction, please feel free to consult our technical team at any time.
Qufu towering power tower Co., Ltd. - a one-stop intelligent manufacturing base for "cement power poles" in China, empowering global power infrastructure construction. We are located in Qufu, Shandong, and are a national high-tech enterprise that integrates the research and development, design, production, and global supply of large-scale concrete power products. We are committed to solving the tedious coordination problems in tower supporting systems for global power and communication engineering, and creating a "full category, one-stop" procurement platform from national standard poles to specialized components. The products are exported in batches to Indonesia, Senegal, Burundi and other countries along the "the Belt and Road", with business covering Southeast Asia, Africa, the Middle East and South America. With strong production capacity reserves and stable batch quality, we have won the trust of multiple state-owned power enterprises for long-term repurchase. We continue to contribute the solid strength of 'Made in China' to global infrastructure construction.
